| Regulatory status of the machine |
21 CFR Part 117.40 |
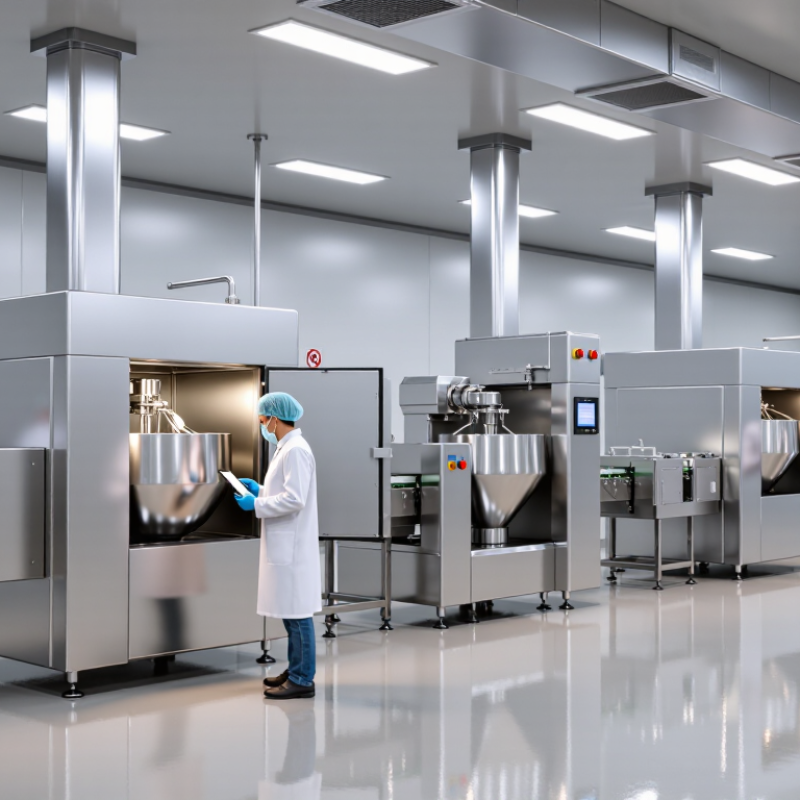
FDA generally does not approve complete food-processing machines as a single product. The equipment must be suitable for use in food manufacturing and must not cause contamination or adulteration. |
Confirm that the machine design, construction, installation, and operating conditions support sanitary food production. |
Equipment specification, sanitary design statement, installation qualification record, and supplier compliance declaration. |
Treat “FDA approved machine” as a compliance claim that must be supported by component-level and design-level evidence. |
| Food-contact material authorization |
21 CFR Parts 174–178; 21 CFR 180–181; FDA Food Contact Notifications |
Each material or substance intended to contact food must have an applicable regulatory basis, such as a listed use in the Code of Federal Regulations, a valid Food Contact Notification, a prior sanction, or another recognized authorization. |
Identify every food-contact material, additive, coating, lubricant, adhesive, gasket, seal, and plastic component. |
Material declaration, applicable CFR citation, Food Contact Notification number where relevant, and supplier letter of compliance. |
Do not accept a general “FDA compliant” statement without identifying the exact material and intended food-contact use. |
| Equipment and utensil design |
21 CFR 117.40(a) |
Equipment and utensils must be adequately cleanable and must be designed, constructed, and used to prevent adulteration of food. |
Review product-contact zones, access points, internal geometry, cleanability, drainage, and inspection access. |
Sanitary design drawings, product-contact-zone drawings, cleanability assessment, and operating instructions. |
Reject designs with inaccessible cavities, unnecessary ledges, dead ends, or areas that cannot be inspected and cleaned. |
| Corrosion-resistant food-contact surfaces |
21 CFR 117.40(a)(1) |
Food-contact surfaces must be made of materials that are corrosion-resistant when exposed to food, cleaning compounds, sanitizing agents, and normal operating conditions. |
Check resistance to the actual product, temperature, pH, salt level, cleaning chemicals, and sanitizer concentration. |
Material certificates, corrosion-resistance data, chemical compatibility chart, and surface-finish specification. |
Select materials based on the complete process environment rather than relying only on a generic stainless-steel designation. |
| Non-toxic and non-reactive surfaces |
21 CFR 117.40(a)(1) and 21 CFR Parts 174–178 |
Food-contact surfaces must be made of non-toxic materials and must not impart color, odor, taste, or harmful substances to food under intended conditions. |
Evaluate potential migration, extractables, flavor impact, and compatibility with the food category and process temperature. |
Migration or extractables testing, intended-use statement, and food-contact compliance declaration. |
Verify the authorization covers the specific food type, temperature, contact time, and use conditions. |
| Plastic components |
21 CFR Part 177, including applicable polymer-specific sections |
Plastic materials must use permitted substances and comply with applicable limitations, specifications, and conditions of use. |
Identify the polymer, colorants, additives, fillers, processing aids, and maximum operating temperature. |
Resin identification, formulation or compliance statement, applicable 21 CFR section, and migration-test results where required. |
Confirm that the authorization applies to repeated-use equipment and the actual food-contact conditions. |
| Rubber, elastomer, and gasket components |
21 CFR 177.2600, where applicable |
Repeated-use rubber articles intended for food contact must meet the applicable extractives and composition requirements under the intended conditions of use. |
Review gasket, O-ring, hose, diaphragm, valve-seat, and seal materials, including temperature and cleaning exposure. |
Elastomer specification, applicable regulatory citation, extractives testing, and replacement schedule. |
Choose seals for the actual product and sanitation chemistry; a seal that swells or cracks can create both contamination and maintenance risks. |
| Lubricants and incidental food contact |
21 CFR 178.3570 |
Lubricants with incidental food contact must meet the applicable requirements and must be used only in permitted applications and quantities. |
Identify every lubricant used near product zones, bearings, chains, gears, seals, and moving assemblies. |
Lubricant technical data sheet, food-contact compliance statement, application instructions, and preventive-maintenance procedure. |
Control lubricant quantity and application points; “food-grade” alone is not a complete regulatory justification. |
| Coatings, paints, and adhesives |
21 CFR Parts 175 and 177, as applicable |
Adhesives, coatings, and polymeric materials used in or near food-contact areas must have an appropriate regulatory basis and must not deteriorate under intended conditions. |
Check whether the coating or adhesive is directly food-contacting, behind a functional barrier, or only used outside the product zone. |
Coating or adhesive compliance statement, cure conditions, barrier information, and chemical-resistance data. |
Avoid exposed painted or bonded surfaces in product zones unless their food-contact status and durability are documented. |
| Cleanability and sanitation |
21 CFR 117.35 and 21 CFR 117.40 |
Equipment must be maintained in a sanitary condition and must be cleaned and sanitized at appropriate intervals to prevent contamination. |
Assess clean-in-place or clean-out-of-place procedures, dismantling requirements, inspection points, and sanitation frequency. |
Cleaning and sanitation standard operating procedures, validation or verification records, chemical instructions, and inspection checklist. |
Prefer designs that reduce manual cleaning steps while still allowing verification of all product-contact surfaces. |
| Drainability and liquid retention |
21 CFR 117.40(a) and 21 CFR 117.35 |
Equipment should be designed and installed so that product, water, cleaning solution, and condensate do not accumulate in a way that can cause contamination. |
Inspect horizontal surfaces, hollow frames, piping slopes, low points, drain legs, and areas where moisture can remain after cleaning. |
General arrangement drawings, piping isometrics, slope specifications, drainage test, and post-cleaning inspection procedure. |
Eliminate avoidable water traps and confirm that the machine can be fully drained before production restart. |
| Hollow structures and framework |
21 CFR 117.40(a) |
Equipment design must prevent contamination from internal spaces, condensate, corrosion, or inaccessible areas. |
Check whether tubular frames are fully sealed, continuously welded, or otherwise designed to prevent liquid and pest entry. |
Fabrication drawings, weld details, enclosure specifications, and inspection records. |
Avoid open-ended tubing and unsealed hollow members in or above product-contact and product-exposure zones. |
| Welds and surface finish |
21 CFR 117.40(a); applicable sanitary-design practices |
Product-contact welds and finishes should be smooth, durable, cleanable, and free from pits, cracks, crevices, and excessive roughness. |
Review weld continuity, blending, polishing, surface damage, heat tint, crevices, and areas vulnerable to corrosion. |
Welding procedure, weld inspection report, surface-finish specification, and repair procedure. |
Specify measurable finish and weld requirements instead of accepting only the phrase “sanitary construction.” |
| Separation of product and non-product zones |
21 CFR 117.35 and 21 CFR 117.40 |
The equipment must be arranged and operated to prevent lubricants, condensate, maintenance debris, dirty air, and other contaminants from entering food. |
Review motor, gearbox, hydraulic, pneumatic, electrical, and maintenance locations in relation to exposed product. |
Risk assessment, layout drawing, drip-protection details, air-quality specification, and maintenance procedure. |
Use physical separation, shielding, drip control, and suitable utilities wherever product is exposed. |
| Compressed air and process utilities |
21 CFR 117.40 and 21 CFR 117.80 |
Utilities that contact food or food-contact surfaces must not introduce contamination and must be suitable for the intended process. |
Determine whether compressed air, gas, water, steam, or vacuum directly contacts product or product-contact surfaces. |
Utility-quality specification, filtration plan, water or gas test results, maintenance records, and monitoring procedure. |
Define utility quality by risk and use point rather than applying one generic specification to every utility. |
| Temperature-control capability |
21 CFR 117.80(b) and applicable preventive-control procedures |
Processes must be controlled as necessary to prevent undesirable microbial growth, toxin formation, contamination, or deterioration. |
Verify heating, cooling, holding, freezing, and temperature-monitoring capability for the specific food process. |
Process specifications, calibration records, temperature uniformity data, alarm settings, and corrective-action procedure. |
Buy sufficient control accuracy and monitoring capability to support the facility’s hazard analysis and preventive controls. |
| Instrumentation and calibration |
21 CFR 117.40 and 21 CFR 117.165 |
Instruments and controls used to monitor preventive controls must be accurate, maintained, and calibrated or checked as appropriate. |
Review sensors, scales, timers, pressure gauges, metal detectors, checkweighers, and data-recording functions. |
Calibration certificates, calibration intervals, verification records, alarm test records, and electronic data-retention procedure. |
Ensure critical measurements can be traced to a defined calibration standard and that failures trigger documented action. |
| Allergen and cross-contact control |
21 CFR 117.80 and 21 CFR 117.135 |
Equipment and processes must be managed to prevent unintended allergen cross-contact and contamination between products. |
Evaluate dismantling, flush capability, line clearance, changeover time, residue removal, and shared-contact surfaces. |
Allergen risk assessment, validated or verified cleaning procedure, changeover checklist, and swab or visual-inspection records. |
Select equipment that supports effective changeovers and makes residual product easy to detect and remove. |
| Pest and environmental contamination control |
21 CFR 117.35(c) and 21 CFR 117.20 |
Equipment and its installation must not create conditions that allow pests, condensate, dust, sewage, or other environmental contaminants to affect food. |
Inspect clearances from floors and walls, access for cleaning, overhead structures, doors, covers, and exposed-product protection. |
Installation drawing, environmental-monitoring plan, pest-control assessment, and equipment-location approval. |
Assess the machine as part of the entire hygienic zoning and facility layout, not as an isolated unit. |
| Preventive-controls integration |
21 CFR Part 117, Subpart C |
Covered facilities must identify and control reasonably foreseeable hazards through a written food-safety plan and preventive controls. |
Determine how the machine supports hazard analysis, process controls, sanitation controls, allergen controls, monitoring, and corrective actions. |
Hazard-analysis input, process-flow diagram, critical or preventive-control parameters, monitoring interface, and corrective-action records. |
Choose equipment that can produce reliable, recordable, and verifiable control data for the facility’s food-safety plan. |
| Traceability and change control |
21 CFR 117.155 and 21 CFR 117.170 |
Preventive-control records and corrective actions must be maintained as required, and significant equipment or process changes must be evaluated for food-safety impact. |
Confirm serial-number tracking, software version control, replacement-part identification, and modification approval procedures. |
Equipment history file, software and firmware records, spare-parts list, change-control form, and maintenance log. |
Require documented change control for materials, seals, coatings, sensors, software, and process-contact components. |
| Supplier qualification |
21 CFR 117.410–117.435, where the machine or component is part of a supplier-control program |
Facilities must use risk-based supplier verification when hazards are controlled through the supply chain or when supplier information supports preventive controls. |
Evaluate the supplier’s technical controls, material traceability, manufacturing records, testing, and nonconformance process. |
Supplier questionnaire, audit report, certificates, test reports, nonconformance history, and approved-supplier record. |
Qualify both the machine supplier and critical component suppliers, especially for food-contact materials and safety-critical controls. |
| Documentation package |
21 CFR Part 117 recordkeeping requirements |
Records should provide objective evidence that the equipment and its operation support applicable preventive controls and sanitary practices. |
Confirm that documents are complete, current, legible, retrievable, and linked to the exact machine configuration. |
Material declarations, drawings, manuals, cleaning procedures, calibration records, validation reports, certificates, and revision history. |
Make document delivery and document revision control contractual purchasing requirements. |
|
Important qualification: The FDA usually regulates the safety and intended use of food-contact substances, manufacturing practices, and facility operations rather than issuing a universal approval certificate for an entire food machine. Final acceptance should be based on the machine’s intended food, process conditions, cleaning chemicals, temperature, contact time, preventive-controls plan, and the applicable requirements in the current edition of the U.S. Code of Federal Regulations.
|
 Chef Nest Kitchen