Explore our elite range of heavy-duty culinary machinery engineered for optimal performance, robust durability, and precision processing in commercial environments.
Built on a foundation of rigorous engineering, industrial mastery, and uncompromising quality standards.
Guangzhou Chef Nest Kitchen Co., Ltd. is a professional manufacturer and supplier specializing in high-quality kitchen appliances and commercial cooking solutions. Located in Guangzhou, Guangdong Province, one of China’s leading industrial and trade hubs, the company benefits from a strategic location with convenient access to domestic and international markets.
Covering an area of over 10,000 square meters, Chef Nest Kitchen operates modern production facilities equipped with advanced assembly lines, quality inspection laboratories, and efficient logistics systems. The company focuses on designing and producing innovative, durable, and user-friendly kitchen products that meet the diverse needs of restaurants, hotels, catering services, and households worldwide.
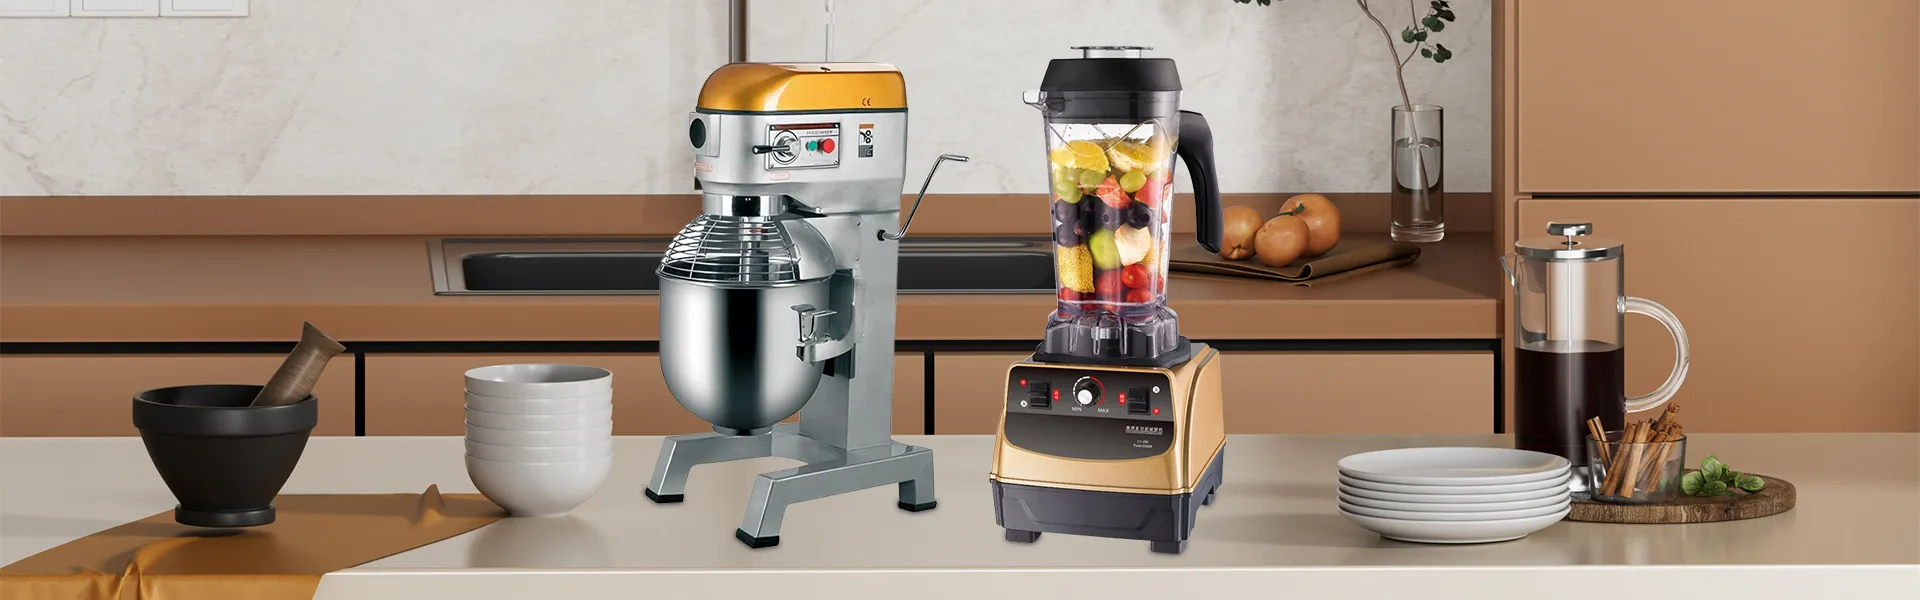
Since its establishment, Guangzhou Chef Nest Kitchen has grown steadily, expanding both its product portfolio and market reach. The company’s offerings include commercial ovens, electric cooking appliances, food processors, beverage machines, and advanced confectionery apparatus designed for efficiency and safety. Over the past decade, Chef Nest Kitchen has invested heavily in research and development.
With a strong emphasis on quality management, the company ensures that every product undergoes rigorous testing before leaving the factory. Guangzhou Chef Nest Kitchen employs over 150 skilled professionals, including engineers, technical specialists, quality inspectors, and sales personnel dedicated to global support.
An authoritative whitepaper perspective on how modern confectionery manufacturing demands unprecedented thermal precision and structural crystal stability.
The worldwide market for commercial chocolate processing machinery has experienced explosive compound annual growth, driven by the surge of artisan chocolatiers, boutique patisseries, and automated industrial confectioners requiring precise crystal control (Form V crystals) for glossy appearance and clean snap.
Next-generation tempering equipment integrates intelligent PLC touch-screens, PID closed-loop heating controls, continuous seeding systems, and variable-speed auger agitation to eliminate thermal hysteresis and guarantee flawless viscosity across diverse cocoa butter matrices.
From high-humidity tropical confectioneries to dry alpine bakeries, localized thermal management modules adapt cooling air currents and jacketed fluid flows to maintain absolute stability regardless of ambient facility climatic fluctuations.
Strategic engineering frameworks designed to future-proof commercial confectionery operations and scale manufacturing capacity.
Modern industrial kitchens require seamless synchronization between melting vats, tempering units, enrobing lines, and cooling tunnels. Our macro solutions provide IoT-enabled telemetry, allowing plant supervisors to monitor batch temperatures, energy consumption, and mechanical wear in real-time via centralized cloud dashboards, drastically reducing downtime and minimizing raw material waste.
As global energy standards tighten, Chef Nest Kitchen leads the industry in eco-conscious thermal engineering. Utilizing advanced heat exchangers, inverter-driven refrigeration compressors, and superior thermal insulation, our equipment slashes electricity consumption by up to 35% while maintaining hyper-accurate thermal stability required for premium couverture chocolate processing.
Discover our specialized high-speed cutters, deep fryers, rotary ovens, and precision milling systems built for high-output commercial bakeries and food factories.
Expert answers regarding our manufacturing standards, customization capabilities, and global logistical support.
 Chef Nest Kitchen