Precision-engineered solutions manufactured under strict ISO9001 and CE standards
Analyzing thermal efficiency shifts, steam generator design, and procurement trends in mass catering
In modern commercial food service and large-scale industrial catering, the demand for high-efficiency, energy-saving, and thermodynamically optimized commercial rice steamers has reached an unprecedented peak. Traditional direct-heating boilers are rapidly being phased out across North America, Europe, the Middle East, and Southeast Asia in favor of intelligent micro-computerized steam generators equipped with multi-stage heat recovery systems.
As top-tier China rice steamer manufacturers lead this transformation, the focus has shifted from basic thermal heating to precise pressure management, atmospheric steam saturation controls, and automated moisture distribution. This technological leap guarantees consistent gelatinization of grain starches, maintaining texture and nutrient retention while dropping energy consumption by up to 34% compared to legacy equipment.
Modern commercial kitchens operate under strict total cost of ownership (TCO) metrics. High-performance steam cookers now integrate smart steam-on-demand valves and food-grade SUS304/SUS316 double-walled insulated bodies to eliminate ambient heat loss.
Thermal conversion rate efficiency in Chinese Smart Industrial Rice Steamers vs Standard Legacy Units:
How overseas procurement directors evaluate industrial food machinery suppliers in China
Global chain buyers require rigorous compliance certifications including CE, ETL, RoHS, and ISO9001 quality management systems. Commercial steaming equipment must pass stringent electrical safety inspections, electromagnetic compatibility (EMC) testing, and pressure vessel stress diagnostics before entering North American and European logistics channels.
Corrosion-resistant SUS304 and SUS316 stainless steels are non-negotiable for high-moisture commercial steam cooking environments. Premium rice steamer factories utilize seamless laser welding to eradicate micro-crevices where bacteria accumulate, complying fully with HACCP hygiene directives for institutional kitchens.
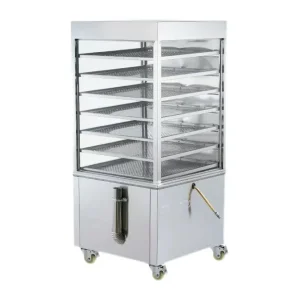
Enterprises require customized tray capacities (ranging from 6-tray breakfast units to 36-tray heavy-duty central kitchen cabinets), adaptable dual-fuel burner systems (natural gas, LPG, or high-voltage electric heating elements), and custom PLC touchscreens capable of storing localized cooking algorithms.
China's commercial kitchen equipment manufacturing hub in Guangdong integrates raw material processing, precision laser cutting, automated stamping, and smart robotic welding into a frictionless ecosystem.
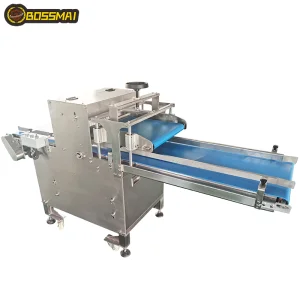
By leveraging localized industrial clusters, top-tier factories achieve unparalleled production speed, agile prototyping, and stringent quality control. This ecosystem allows manufacturers to deliver high-capacity commercial steamers, jacketed mixing kettles, food grinders, and dough processing systems with minimized lead times and optimized cost structures.
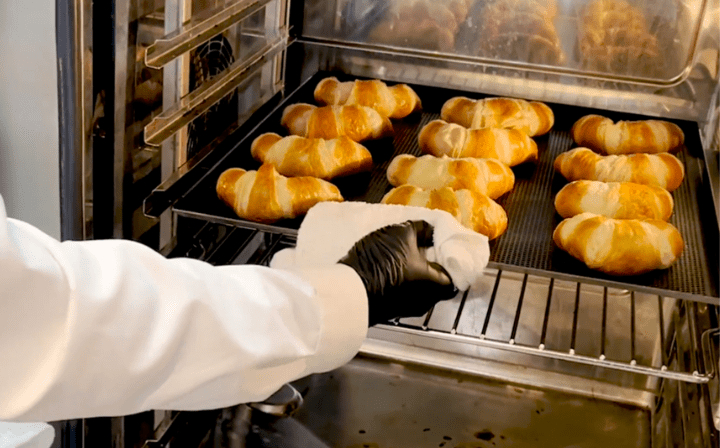
Optimized engineering workflows tailored for diverse hospitality and food manufacturing segments
For school cafeterias, hospital dietary units, and military catering, large multi-trolley roll-in steam cabinets ensure high-volume continuous output. They deliver thousands of portions of uniformly cooked rice, steamed buns, and root vegetables while reducing direct labor overhead by up to 40%.
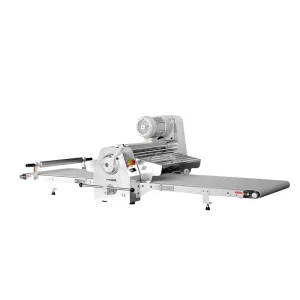
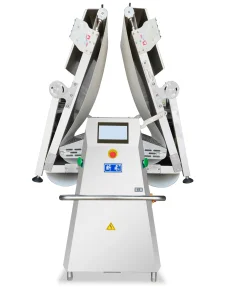
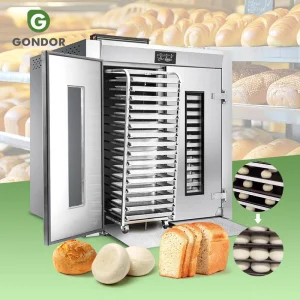
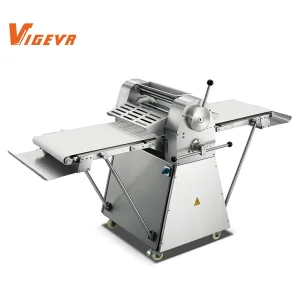
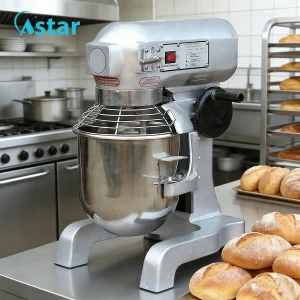
Steam cookers and proofing cabinets work in tandem with industrial dough sheeters and spiral mixers. Precision humidity and heat control in steam proofers allow optimal yeast activation and dough expansion prior to high-capacity deck or convection oven baking.
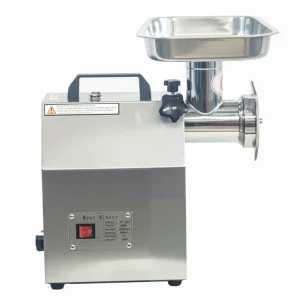
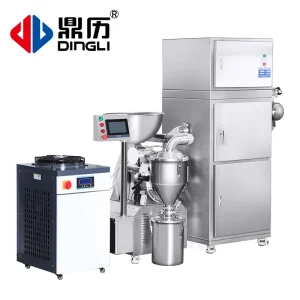
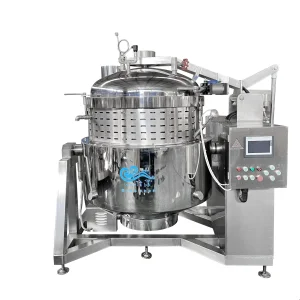
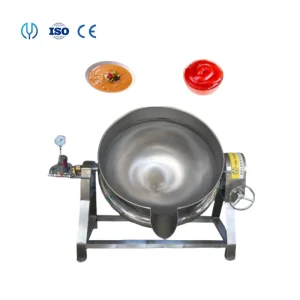
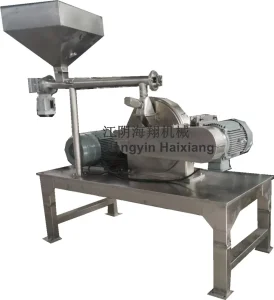
Integrated food processing lines pair high-pressure steam jacketed kettles for sauce cooking with high-efficiency spice pin mills and herbal powder grinders, enabling mass preparation of ready-to-eat meal kits and industrial spice blends.
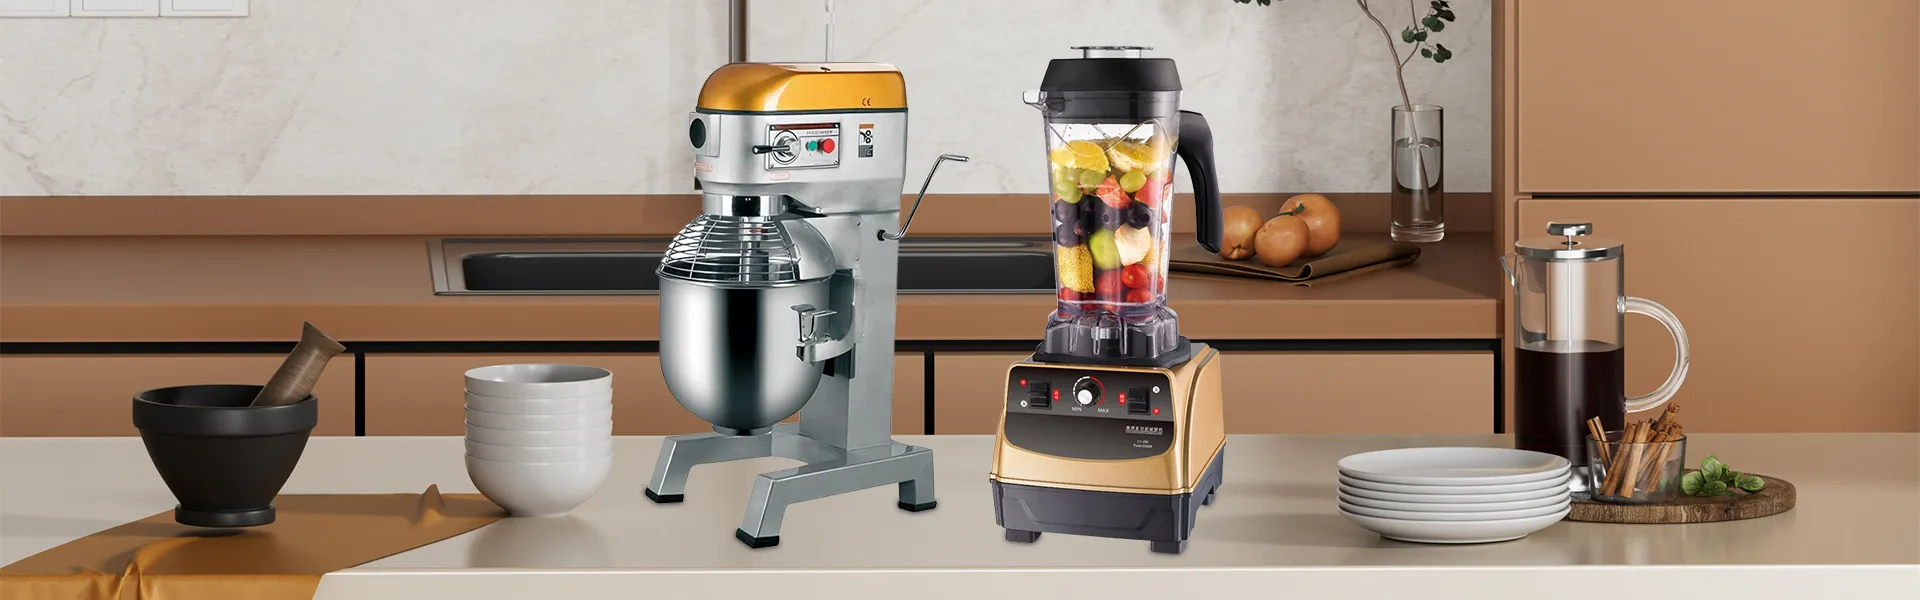
Guangzhou Chef Nest Kitchen Co., Ltd. is a professional manufacturer and supplier specializing in high-quality kitchen appliances and commercial cooking solutions. Located in Guangzhou, Guangdong Province, one of China’s leading industrial and trade hubs, the company benefits from a strategic location with convenient access to domestic and international markets. Covering an area of over 10,000 square meters, Chef Nest Kitchen operates modern production facilities equipped with advanced assembly lines, quality inspection laboratories, and efficient logistics systems. The company focuses on designing and producing innovative, durable, and user-friendly kitchen products that meet the diverse needs of restaurants, hotels, catering services, and households worldwide.
Since its establishment, Guangzhou Chef Nest Kitchen has grown steadily, expanding both its product portfolio and market reach. The company’s offerings include commercial ovens, electric cooking appliances, food processors, beverage machines, and other kitchen equipment designed for efficiency and safety. Over the past decade, Chef Nest Kitchen has invested in research and development, enabling it to launch a series of products that combine smart functionality, energy efficiency, and ergonomic design. With a strong emphasis on quality management, the company ensures that every product undergoes rigorous testing before leaving the factory.
Guangzhou Chef Nest Kitchen employs over 150 skilled professionals, including engineers, technical specialists, quality inspectors, and sales personnel. This team is dedicated to providing exceptional customer service and technical support to clients worldwide. Guided by principles of innovation, reliability, and customer satisfaction, Guangzhou Chef Nest Kitchen Co., Ltd. continues to expand its global footprint, offering trusted kitchen solutions and building long-term partnerships with distributors, restaurants, and catering enterprises in multiple regions.
Addressing core engineering, custom options, and logistics inquiries from procurement teams
Explore our comprehensive industrial catalog designed for global commercial kitchens
 Chef Nest Kitchen